
Key Takeaways
- 24/7 Demands: Healthcare kitchens require connected, reliable equipment to sustain continuous production and strict food safety across all shifts.
- Integrated Workflows: Combining Retigo combi ovens, Irinox blast chillers, Continental pass-thru refrigeration, MEIKO warewashing, and Mercer allergen tools creates a seamless operational flow.
- Hands-On Evaluation: High Sabatino Associates supports Mid-Atlantic healthcare facilities with live demonstrations at our Jessup, MD test kitchen and our mobile test kitchen.
Healthcare foodservice operates on a different clock.
Hospitals, senior living communities, rehabilitation centers, and other healthcare facilities feed patients, residents, visitors, and employees throughout the day. Dietary requirements vary widely, food safety is critical, and production does not stop after the lunch or dinner rush.
That puts unique pressure on the kitchen.
Equipment needs to support consistent production, safe food handling, efficient workflows, and staff working across multiple shifts. When one part of that process slows down, the effects reach far beyond a single meal period. The answer is rarely more equipment. It’s equipment that works together.
Across Maryland, Washington, D.C., Virginia, and West Virginia, High Sabatino Associates works with healthcare foodservice operators, dealers, consultants, and designers to identify equipment solutions that fit the way an operation actually functions.
This October, as the industry celebrates Healthcare Foodservice Workers Week, we’re especially grateful for the teams who keep those kitchens running every hour of every day.
Plan Production Around the Clock
Healthcare kitchens may produce hundreds of meals while accommodating specialized diets, different textures, and varied service schedules.
Retigo Vision combi ovens combine hot air, steam, and combination cooking in one platform, helping healthcare kitchens handle a broad range of production needs with consistent results across employees and shifts.
Retigo’s steam generation system creates saturated steam that helps preserve color, texture, flavor, and nutrients, an important consideration for patient meals. Active Humidity Control automatically manages moisture during cooking, and an overnight cooking function lets kitchens put the oven to work during quieter hours.
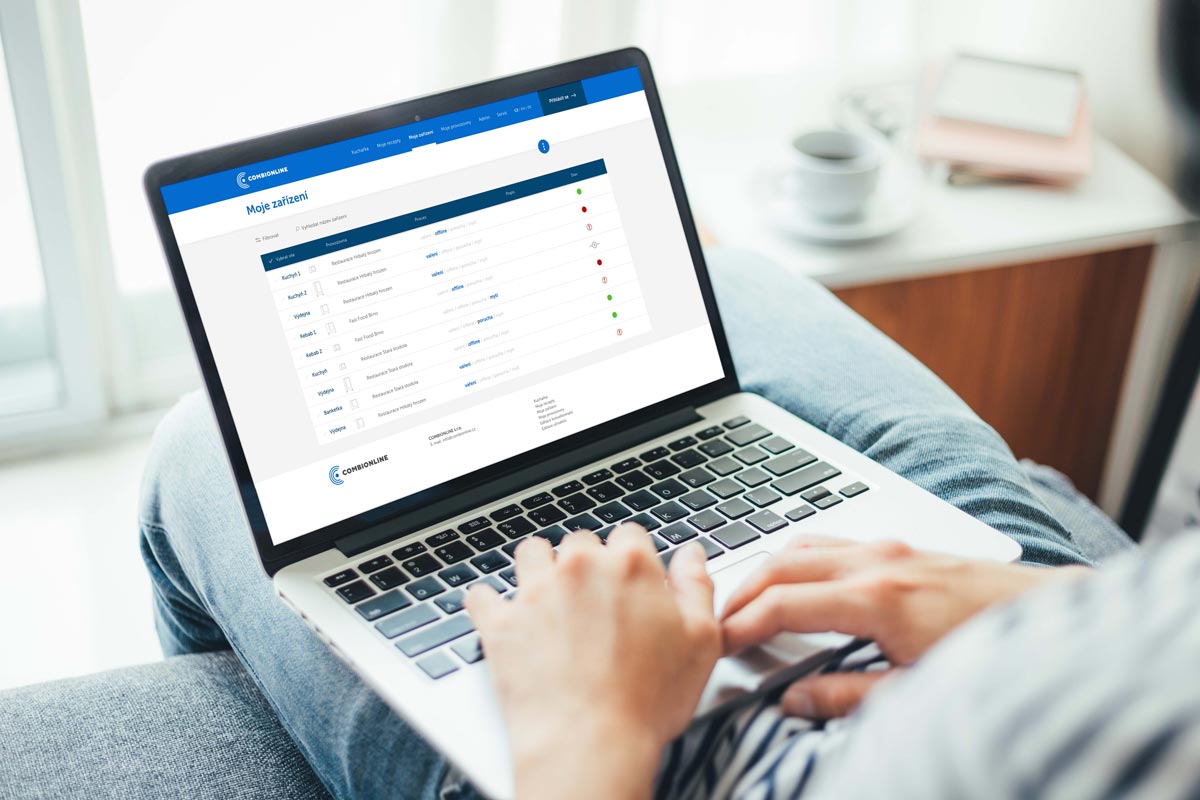
The touchscreen controls respond accurately even when staff wear gloves, which helps cut training time for teams working across multiple shifts. Retigo’s Combi Online platform connects the oven to your network, so managers can update recipes, check cooking status, and download operating data from a phone, tablet, or laptop. HACCP records, operating logs, and error history all live in one place, and the system can alert your team and service partner if a machine goes down, which matters when downtime isn’t an option.
For healthcare operations, that combination of versatility, consistency, and ease of use can simplify production throughout the day.
Build a Safer Cook-Chill Process
In healthcare foodservice, safely managing food between cooking and service is critical, especially when kitchens produce meals in large batches or ahead of time.
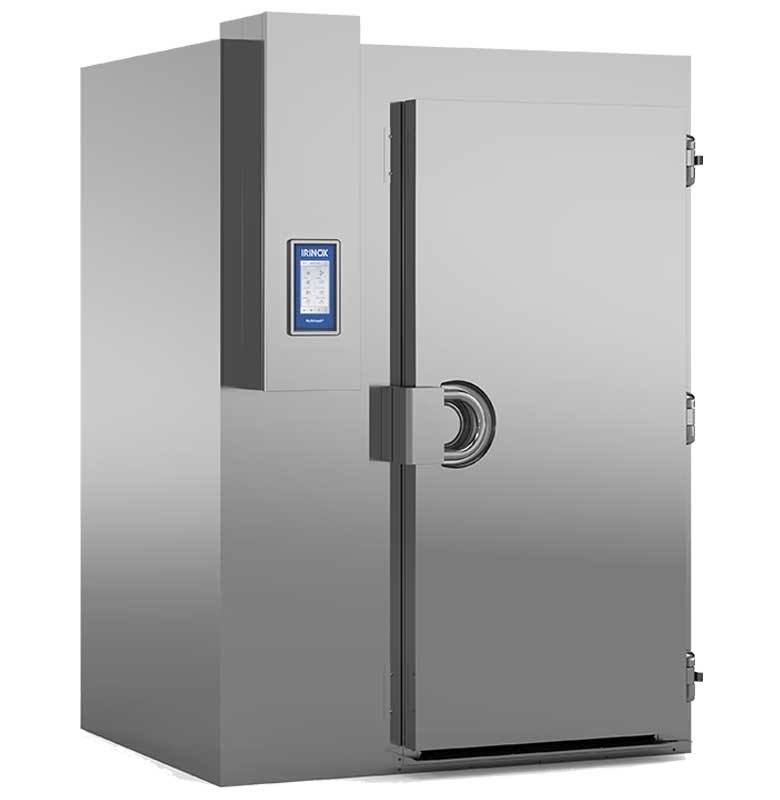
Irinox blast chillers bring the core of freshly cooked food down to 37°F, even from boiling hot, helping healthcare kitchens follow HACCP food safety protocols while preserving food quality. Kitchens can prepare meals in larger batches, chill them rapidly, store them safely, and regenerate them later for service, which helps teams manage labor across the day.
For high-volume hospital kitchens, the MultiFresh MyA 130.2 roll-in chills or freezes up to 287 pounds per cycle and accepts a full rolling cart. Its low-temperature cooking cycle can run overnight and switch automatically to chilling as soon as cooking finishes, so the next day’s meals are ready when the morning shift arrives.
Smaller facilities, like senior living communities and rehabilitation centers, can turn to the MultiFresh Next reach-in line, with blast chilling capacities from 55 to 154 pounds per cycle. Each unit includes Irinox’s Sanigen automatic sanitization system, which Irinox says eliminates 99.5% of the bacterial load inside the product chamber. FreshCloud connectivity lets managers monitor cycles remotely, receive push notifications, and back up HACCP data.
Keep Cold Storage Close to the Workflow
From the first shift to the last, the refrigerator door in a healthcare kitchen hardly stays shut. Reliable cold storage keeps ingredients and prepared foods at safe temperatures from one shift to the next.
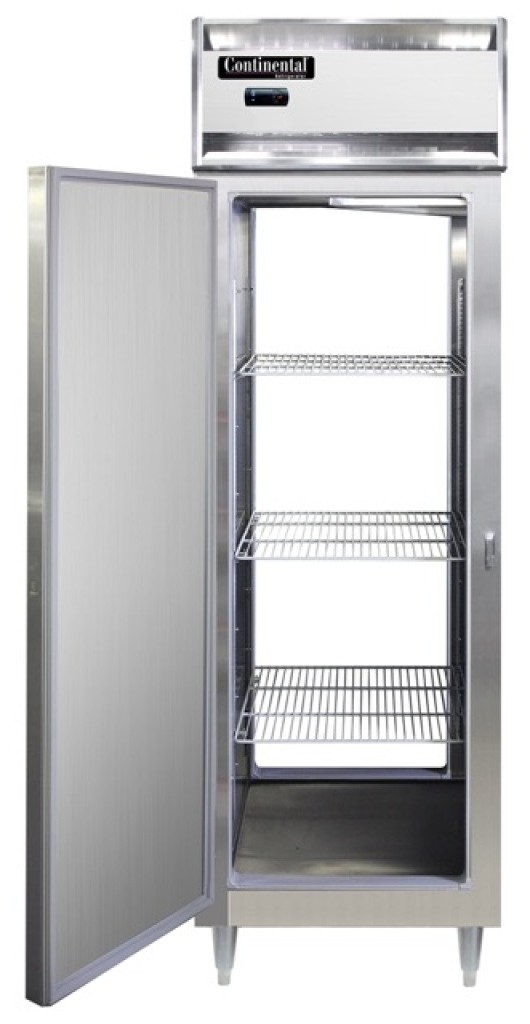
Continental Refrigerator builds reach-in and pass-thru refrigerators and freezers in one, two, and three sections, in various widths and depths, with door options including solid, half, and glass doors. That flexibility lets operators match each unit to its spot in the workflow.
Pass-thru models deserve a close look in healthcare. Production staff can load prepared items from one side while tray assembly or service staff pull from the other, keeping two teams out of each other’s way during busy meal periods.
Continental’s pass-thru units also include an electronic controller with a digital display, self-closing doors, and a refrigeration system mounted on top of the cabinet, readily accessible and separate from the food zone. That last detail matters to the facilities team that keeps the unit running.
Keep Up with Around-the-Clock Warewashing
Healthcare foodservice generates a steady flow of patient meal trays, cafeteria dishes, utensils, insulated covers, pots, and pans that staff need to clean and return to service.
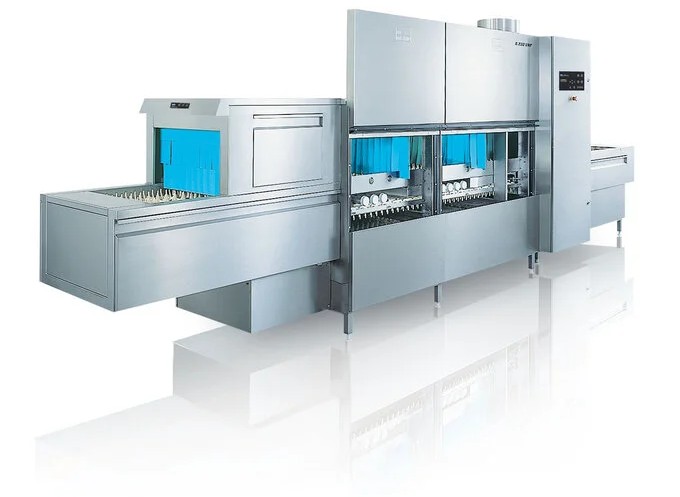
For high-volume tray and dish return, the MEIKO M-iQ flight type dishwasher keeps washware moving on a continuous conveyor. Its high passing entry height accommodates hospital dishes, insulated boxes, and trays, so a single machine can handle the full mix coming back from patient floors and the cafeteria.
Production items create a different challenge. The MEIKO FV 130.2 pot and pan washer handles bulky washware like pots, pans, trays, and containers, and its large basket holds up to 11 sheet pans, moving that work out of the sink and into an automated wash process.
MEIKO also makes cleaning and disinfection equipment designed for hospitals and care homes, including washer-disinfectors for bedpans, urine bottles, and other care utensils.
For facilities serving patients, visitors, and employees around the clock, reliable warewashing helps maintain hygiene, supports staff, and keeps clean items returning to service.
Make Allergen-Safe Prep Easy to Spot
Healthcare kitchens often manage food allergies, gluten-free diets, and other specialized dietary needs, which makes clear cross-contamination procedures especially important.
Mercer Culinary’s Allergen Safe and Designated Gluten Safe lines use purple, the industry standard color for allergen-free food prep, so staff can identify dedicated tools at a glance. The lineup covers nearly every prep task, from chef’s, Santoku, bread, boning, and paring knives to turners, pie servers, spreaders, a bench scraper, and silicone bake mats. The knives and most prep tools carry the NSF mark, and the Hell’s Tools mixing spoon, slotted spatula, and utility tongs handle temperatures up to 430°F.
To keep everything together, the Mercer Allergen Safety Set packs the full collection into a dedicated purple storage tote, so allergen-safe tools stay separate from the rest of the kitchen’s equipment.
High Sabatino offers Mercer Culinary through Ware Necessities, our tabletop and supplies division.
For healthcare teams working across multiple meals and shifts, a simple visual system makes allergen safety procedures easier to recognize and follow.
Looking Ahead
Keeping healthcare foodservice running around the clock takes more than dependable individual pieces of equipment. It takes a connected workflow.
Cooking equipment supports consistent production. Blast chilling gives kitchens flexibility around when they prepare food while supporting food safety. Refrigeration protects products and keeps them close at hand. Warewashing keeps clean items returning to service. And everyday prep tools help staff follow allergen safety procedures consistently.
At High Sabatino Associates, we’re proud to represent manufacturers like Retigo, Irinox, Continental Refrigerator, MEIKO, and Mercer Culinary that address different parts of that workflow.
The right solution looks different for every healthcare facility. That is why the process should begin with the operation itself: its menu, meal volume, staffing, dietary requirements, available space, and the points where work slows down.
Evaluate Healthcare Foodservice Equipment in the Mid-Atlantic
Equipment decisions get easier when operators can look beyond a spec sheet and see how a solution fits their actual needs.
High Sabatino Associates works with healthcare foodservice professionals, dealers, consultants, and designers throughout Maryland, Washington, D.C., Virginia, and West Virginia to evaluate equipment around real operational challenges.
Our 4,500 sq. ft. demonstration kitchen in Jessup, Maryland, gives you a place to see equipment in action, discuss workflows, and evaluate solutions before committing to a major purchase. Can’t step away from a 24/7 operation? Our mobile test kitchen brings live demonstrations to your facility.
We also host live demo events throughout the year, like the three days of Retigo cooking demonstrations we held in September. Visit our Events page to see what’s coming up next.
Bring your menu, production volume, staffing concerns, and workflow challenges, and invite your facilities team along. Our team can help identify where the operation slows down and explore equipment that fits the way your healthcare kitchen needs to work.
Because in healthcare, the kitchen never gets a day off. Your equipment shouldn’t either.
Ready to see what a more connected workflow could look like? Contact High Sabatino Associates to schedule a visit to our Jessup test kitchen or ask about bringing our mobile test kitchen to you.
Frequently Asked Questions
What equipment does a healthcare foodservice operation need?
A healthcare foodservice operation requires dependable cooking, refrigeration, chilling, warewashing, and prep solutions designed to support continuous 24/7 production and strict food safety standards.
How can a combi oven help a healthcare kitchen?
A combi oven supports repeatable production by combining multiple cooking methods into a single programmable platform, simplifying meal preparation across multiple shifts and staff members.
Why would a healthcare kitchen use a blast chiller?
A blast chiller rapidly lowers the core temperature of freshly cooked food to support food safety protocols and give kitchen staff flexible batch-cooking capabilities.
How can healthcare kitchens support allergen safety?
Healthcare kitchens maintain allergen safety by implementing strict cross-contamination protocols and using dedicated, color-coded tools like Mercer Culinary’s Allergen Safe line.
How do I choose healthcare foodservice equipment for a 24/7 operation?
Choosing equipment for a 24/7 operation starts with analyzing your menu, meal volume, shift staffing, and workflow bottlenecks rather than evaluating spec sheets in isolation.
Ready to see what a more connected workflow could look like?
Contact High Sabatino Associates to schedule a visit to our 4,500 sq. ft. demonstration kitchen in Jessup, Maryland, or ask about bringing our mobile test kitchen directly to your facility. Bring your menu, production volume, and workflow challenges, and let our team help your 24/7 operation run more smoothly.
